The Hidden Power of Tool Center Point: Mastering Precision in Modern Workflows
Precision in manufacturing isn’t just about the machine—it’s about the invisible reference point where every measurement begins. That point is the tool center point (TCP), the geometric heart of every cutting tool, robotic end-effector, or probing system. Without its exact calibration, even the most advanced CNC mills or collaborative robots would produce parts with inconsistent tolerances, wasting material, time, and reputation. The TCP isn’t just a technical specification; it’s the silent arbiter of accuracy in industries where fractions of a millimeter determine success or failure.
Yet for many operators, the concept remains shrouded in ambiguity. Questions linger: What exactly is the tool center point? Is it the tip of a drill bit, the center of a milling cutter, or something more abstract? And why does a seemingly minor adjustment—like shifting the TCP by 0.1mm—ripple through an entire production run? The answers lie in the intersection of geometry, physics, and industrial engineering, where theory meets the cold reality of shop floors. Understanding these principles isn’t optional; it’s the difference between a part that fits and one that doesn’t.
The stakes are higher than ever. As industries adopt Industry 4.0 technologies—where machines self-calibrate and AI optimizes toolpaths—the role of the TCP evolves from a static calibration point to a dynamic variable in real-time control systems. But before exploring its future, we must first grasp its fundamentals: the invisible axis around which modern manufacturing pivots.

The Complete Overview of What Is Tool Center Point
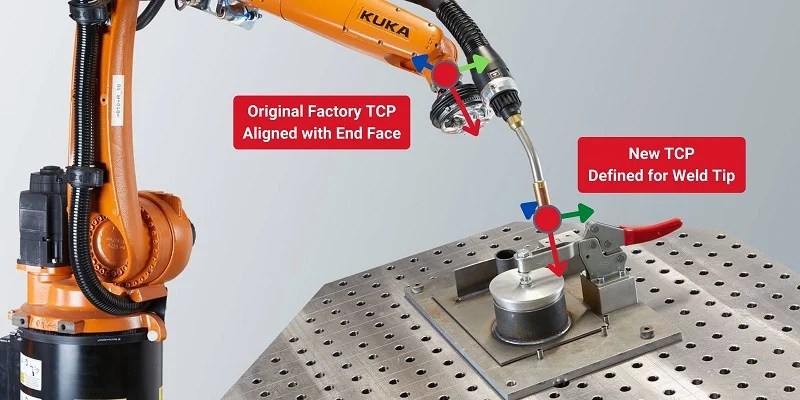
The tool center point (TCP) is the precise geometric reference used to define the position and orientation of a cutting tool, probe, or robotic end-effector in a coordinate system. In practical terms, it’s the point in space that a machine control system treats as the "active" part of the tool—whether that’s the tip of a drill, the center of a milling cutter’s cutting face, or the contact point of a tactile sensor. When a CNC machine executes a command like "G0 X10 Y20," it’s not moving the tool’s shank or holder; it’s moving the TCP to those coordinates. This distinction is critical because the physical tool often extends beyond or behind this point, requiring compensation for accurate material removal.What makes the TCP concept complex is its dual nature: it’s both a physical reality and an abstract model. The actual TCP may not exist as a tangible feature on the tool—especially in cases like ball-nose end mills, where the "center point" is a calculated intersection of the tool’s geometry. Manufacturers and programmers must account for this through tool definitions, offsets, and calibration routines. For example, a 10mm diameter drill’s TCP is theoretically at its tip, but in practice, the machine’s control system may need a 5mm offset if the toolholder adds length. This offset is stored as a tool length compensation (TLC) value, directly tied to the TCP’s definition.
Historical Background and Evolution
The origins of the TCP trace back to the early days of numerical control (NC) machining, when engineers grappled with translating human-readable blueprints into machine-readable instructions. Before CNC systems, operators manually adjusted tools using dial indicators and templates—a process prone to human error. The introduction of the TCP in the 1960s and 1970s marked a shift toward standardized references. Early NC machines treated the TCP as a fixed point relative to the toolholder, but as tools grew more complex (e.g., indexable inserts, multi-axis milling), the need for dynamic TCP definitions emerged.The 1980s and 1990s saw the TCP evolve into a programmable parameter, thanks to advancements in computer numerical control (CNC). Manufacturers like Haas and Fanuc developed systems where operators could define TCPs for different tool types, including offsets for toolholders, collets, and even wear compensation. This era also introduced the concept of tool touch-off, where a probe physically locates the TCP by contacting a reference surface, automating what was once a manual process. The rise of CAD/CAM integration in the 1990s further cemented the TCP’s role, as software could now generate toolpaths with embedded TCP data, reducing setup errors.
Core Mechanisms: How It Works
At its core, the TCP operates through a combination of geometric modeling and real-time feedback. When a tool is installed in a machine, its TCP is defined in the control system’s tool table, which includes:1. Tool geometry (e.g., diameter, flute length, tip angle).
2. Offset values (compensating for the toolholder’s length or angle).
3. Wear compensation (adjusting for tool degradation over time).
Table of Contents
- The Complete Overview of What Is Tool Center Point
- Historical Background and Evolution
- Core Mechanisms: How It Works
- Key Benefits and Crucial Impact
- Major Advantages
- Comparative Analysis
- Future Trends and Innovations
- Conclusion
- Comprehensive FAQs
- Q: What is the difference between a tool center point and a tool length offset?
- Q: How often should TCP calibration be performed?
- Q: Can a TCP be defined for non-cutting tools, like probes or grippers?
- Q: What happens if the TCP is misaligned by 0.1mm in a CNC machine?
- Q: How do CAD/CAM systems handle TCP data?
- Q: Are there industry standards for TCP calibration?
- Q: Can a TCP be dynamically adjusted during machining?
For example, a ball-nose end mill’s TCP isn’t at its physical tip but at the center of the spherical radius. The control system calculates this point using the tool’s CAD model and applies it during machining. During operation, the machine’s servo motors position the TCP along the programmed path, while the tool’s physical body follows at a calculated distance. This separation is why a single G-code command can produce intricate 3D surfaces without manual intervention.
The TCP’s accuracy hinges on calibration. Methods include:
Even minor misalignments—such as a 0.05mm error in a TCP’s Z-axis—can lead to scrap parts in precision applications like aerospace or medical device manufacturing.
Key Benefits and Crucial Impact
The TCP isn’t just a technicality; it’s the linchpin of repeatability in automated manufacturing. Without a stable reference point, machines would struggle to replicate parts with tight tolerances, forcing operators to rely on costly manual adjustments. Industries like automotive, aerospace, and electronics depend on TCPs to maintain consistency across production runs, reducing rework and waste. The impact extends beyond accuracy: a well-defined TCP enables faster setup times, as machines can automatically compensate for tool changes or wear, minimizing downtime.The TCP’s role in modern workflows is underscored by its integration with advanced technologies. In additive manufacturing, for example, the TCP defines the build platform’s reference for layer-by-layer deposition. In robotics, collaborative arms use TCPs to interact safely with human operators or delicate materials. Even in quality inspection, coordinate measuring machines (CMMs) rely on TCP definitions to probe parts with micrometer precision. The quote below captures its essence:
"The tool center point is the silent architect of precision—an invisible axis around which the entire manufacturing process rotates. Master it, and you master the machine." — Dr. Elena Voss, Director of Metrology at MIT’s Precision Engineering Lab
Major Advantages
Understanding and optimizing the TCP offers tangible benefits across manufacturing operations:- Enhanced Part Accuracy: Eliminates discrepancies between programmed and actual tool positions, ensuring parts meet design specifications within ±0.005mm in high-end applications.
- Reduced Setup Time: Automated TCP calibration (e.g., via ATS systems) cuts tool-change times by up to 70%, improving shop floor efficiency.
- Wear Compensation: Dynamic TCP adjustments counteract tool degradation, extending tool life and reducing material waste.
- Multi-Axis Flexibility: Enables complex toolpaths in 4th/5th-axis machining by dynamically recalculating TCP positions relative to the workpiece.
- Regulatory Compliance: Critical for industries with strict tolerances (e.g., ISO 2768 for mechanical parts), where TCP errors can lead to product recalls.
Comparative Analysis
Not all TCPs are created equal. The table below compares key aspects of TCP definitions across different tool types and applications:| Tool Type | TCP Definition and Challenges |
|---|---|
| Drills | The TCP is typically the tip, but runout or chatter can shift it. Requires frequent touch-off for accuracy. |
| End Mills | Ball-nose mills use the sphere’s center; square-end mills use the tip. Wear on flutes alters the effective TCP. |
| Turning Tools | TCP is the cutting edge’s active point. Insert wear shifts it, necessitating dynamic compensation in live tooling. |
| Probes/Sensors | TCP is the contact point (e.g., stylus tip). Requires high-resolution calibration for CMM or in-process measurement. |
Future Trends and Innovations
The TCP is poised to become even more dynamic with the advent of smart manufacturing. Emerging trends include:The integration of 5G and edge computing will further blur the line between physical and digital TCPs, enabling cloud-based calibration and collaborative robotics where multiple TCPs (e.g., from a robot and a CNC) must synchronize seamlessly. As industries adopt these innovations, the TCP will shift from a static calibration point to a living parameter—one that evolves alongside the machine’s state.

Conclusion
The tool center point is more than a technical specification; it’s the foundation upon which modern manufacturing stands. Its proper definition and calibration separate high-volume production from costly errors, and its future will be shaped by how well industries leverage data and automation to keep it precise. For operators, engineers, and technicians, mastering the TCP isn’t just about understanding a concept—it’s about embracing a mindset where precision is non-negotiable.As machines grow more autonomous, the TCP’s role will expand beyond calibration to include predictive maintenance, adaptive control, and even self-optimizing workflows. Those who treat it as an afterthought risk falling behind; those who treat it as the cornerstone of their operations will lead the next wave of industrial innovation.
Comprehensive FAQs
Q: What is the difference between a tool center point and a tool length offset?
The tool center point (TCP) is the geometric reference for the tool’s active position, while the tool length offset (TLO) is the compensation value applied to align the TCP with the machine’s coordinate system. For example, a 50mm toolholder may require a -50mm TLO to position the TCP correctly. The TCP defines where the tool acts; the TLO defines how to reach that point.
Q: How often should TCP calibration be performed?
Frequency depends on usage and tool type. High-wear tools (e.g., drills, end mills) may need daily touch-offs, while stable tools (e.g., solid carbide inserts) can be calibrated weekly or monthly. Automated systems with wear monitoring can trigger recalibration dynamically, reducing manual intervention.
Q: Can a TCP be defined for non-cutting tools, like probes or grippers?
Yes. Probes use their contact point (e.g., stylus tip) as the TCP, while robotic grippers define it at the center of the gripping surface. These TCPs are critical for tasks like part inspection or pick-and-place operations, where precision is as vital as in machining.
Q: What happens if the TCP is misaligned by 0.1mm in a CNC machine?
A 0.1mm TCP error can cause parts to exceed tolerances, leading to scrap or rework. In critical applications (e.g., aerospace), this may violate safety standards. The error compounds in multi-axis machining, where even small deviations accumulate across complex toolpaths.
Q: How do CAD/CAM systems handle TCP data?
Modern CAD/CAM software (e.g., Mastercam, NX) imports TCP definitions directly from tool libraries or manufacturer datasheets. These systems generate G-code with embedded TCP offsets, ensuring the machine’s control system knows the tool’s active position without manual input.
Q: Are there industry standards for TCP calibration?
While no single global standard governs TCP calibration, organizations like ISO and ANSI provide guidelines for tool measurement and compensation. For example, ISO 10360 outlines acceptance tests for CMMs, which rely on TCP definitions for accuracy verification.
Q: Can a TCP be dynamically adjusted during machining?
Yes, advanced CNCs and robotics systems use real-time feedback (e.g., from force sensors or vision systems) to adjust the TCP dynamically. This is common in adaptive control machining, where the system compensates for tool wear or workpiece deformation mid-operation.
Leave a Comment
Comments are moderated before appearing. The data you submit is processed according to the Privacy Policy of Gouv.